Rapid Prototyping | Production-Manufacturing Services
Rapid Prototyping | Production-Manufacturing Services
At Galaxy3DM, As we have tried to come up with a strategy and a vision for Galaxy3DM, it started with" what incredible benefits can we give to the customer? Where can we take the customer?" Our company can provide comprehensive services, precision machining, 3D printing, sheet metal, injection molding from prototype processing to surface treatment, extrusion, silicone mold, most of our engineers are more than 10 years of industry experience, we are waiting for you at Seetop Technology, give us your design, we will give you a free quote.


Resin transfer molding is a closed-mold process utilizing matched male and female molds. Molds for RTM processes can be made out of a variety of materials, including steel, aluminum, nickel or composite.
If you need to manufacture large parts with a high strength to weight ratio, resin transfer molding (RTM) might just be the process you need. Resin transfer molding is a form of composite liquid molding in which resin is mixed with a catalyst or hardener before being injected into a closed mold filled with reinforcing fibers.
RTM’s strength, durability and high glass-to-resin ratio make it perfect for creating large, strong parts. In addition, RTM is also a viable option for molding complex shapes, up to and including compound curves.
Galaxy3DM uses a variety of methods to produce FRP parts. Our experienced engineers will select the best method for your project based on factors such as production volume, parts dimensions, budget, and other requirements.Our extensive experience with Light Resin Transfer Moulding (LRTM) enables us to produce innovative and cost effective parts for our OEM customers.The process is best suited for high precision parts where a two-sided finish is required, and for moderate production quantities, ranging from 100 to 7,000 parts per year.
HR RTM
As a variation of the RTM process, HPRTM uses higher injection pressures for the reactive thermoset mixture.

Light RTM
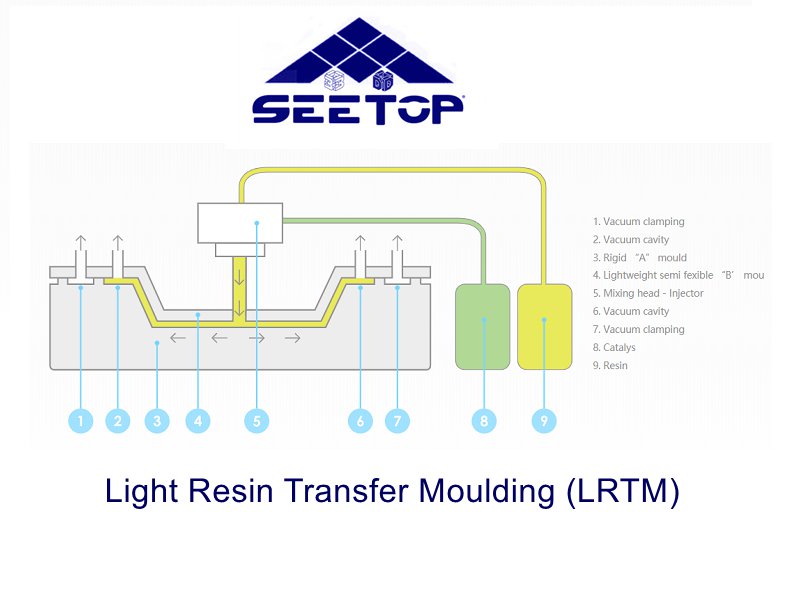
The RTM Light process (also know as LRTM, ECO, Vacuum Molding, VARTM) for fiber reinforced composites, has recently taken the lead as the most popular closed molding process for low to medium volume applications.
VARTM
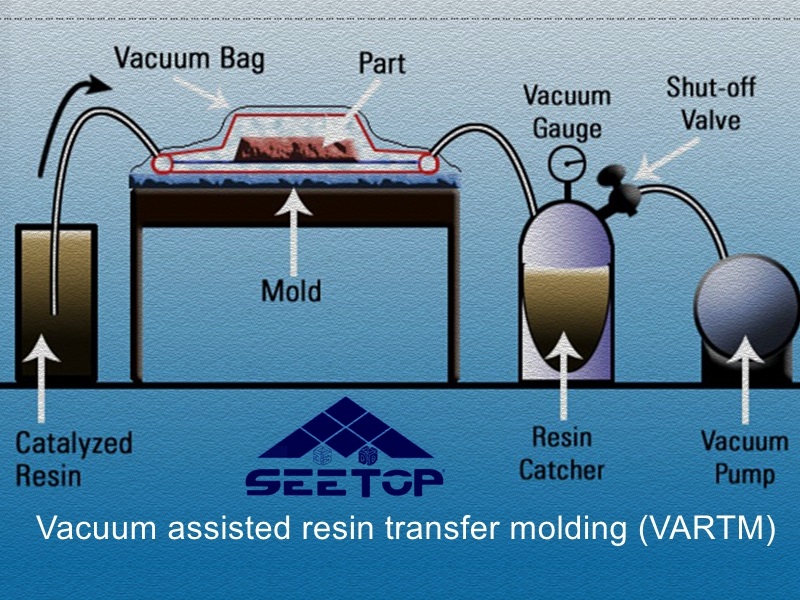
Vacuum assisted resin transfer molding (VARTM) is likely the most common acronym of all used in the discussion of low pressure closed mold reinforced composite molding.
RTM TEHCNOLOGY IN CHINA
As we all know, RTM are wided applied in USA and Europe. In China, more and more factories and specialist show great interests about RTM. Some factories has adopted LRTM into their production of automotive parts. Several brand of RTM machine has been developped by China machine manufacturer.
RTM Machine

RTM Process Machine China

RTM Process Machine China

RTM Process Machine China
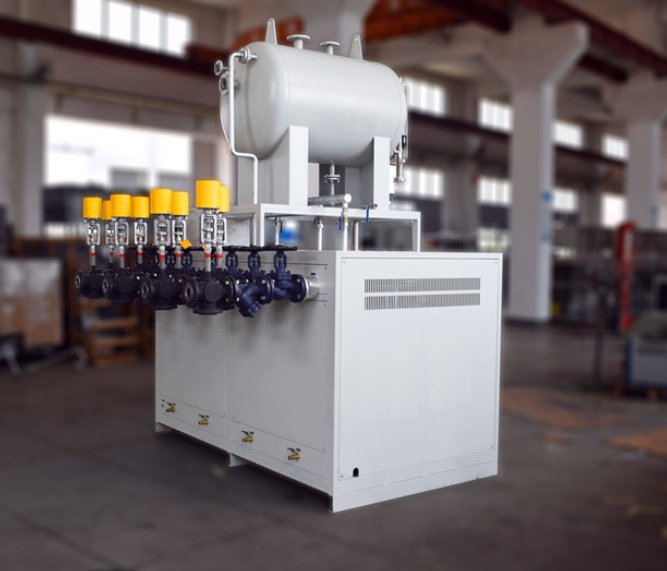
RTM Process Machine China
LRTM PROCESS
LRTM is a closed mould process. The LRTM mould consists of a rigid “A” side mould (base mould) and a lightweight semi-flexible “B” side mould (counter mould) that is sealed to the “A” side mould using vacuum pressure.
Resin is drawn into the resulting cavity under vacuum. The resin infusion may be assisted by a resin injection pump, which will accelerate the infusion process. Once an “A” side mould is cured, the “B” side mould is removed and the part is demoulded from the “A” side mould.
Once the glass reinforcement is fully saturated or “wet out,” the laminate is compacted with specially designed rollers and brushes to remove air bubbles and distribute the resin evenly. Multiple layers, or plies, of laminate are built up in sequence, often with a core material in the middle, to reac h the desired thickness. Various inserts, ribs, fasteners, or other items can be incorporated in the moulded part. Following a curing cycle, the part is de-moulded and trimmed as required.
LRTM production is more efficient than most other processes. You can use a single “B” mould in conjunction with multiple base moulds to achieve production rates of up to three moulded parts per hour. In this case there are three “A” moulds, which move from the mould prep area through the production cycle, while the “B” mould remains in a fixed location.
Its Process mainly include:
1. CREATING THE PREFORM
2. PREFORM LAYUP
3. CLOSING MOLD
4. INJECTION PHASE
5. CURING PHASE
LRTM Materials options
Resins: Generally epoxy, polyester, vinylester and phenolic, although high temperature resins such as bismaleimides can be used at elevated process temperatures.
Fibres: Any. Stitched materials work well in this process since the gaps allow rapid resin transport. Some specially developed fabrics can assist with resin flow.
Cores: Not honeycombs, since cells would fill with resin, and pressures involved can crush some foams.
LRTM Advantage
- LRTM tooling costs are a fraction of the price of equivalent RTM moulds.
- High productivity—mould cycles can be as fast as 20 minutes per part using a single “B” side mould and three “A” side moulds.
- It is possible to achieve cosmetic surfaces on both “A” and “B” side of part.
- High fibre volume laminates can be obtained with very low void contents.
LRTM Limitations
-
The process is generally limited to smaller components
- Not suitable for parts with negative draft
- Part thickness is fixed at the time of mould construction
- Glass-resin ratios of less than 35%
LRTM Application
- 1.Complex aircraft and automotive components
- 2.Train seats
- 3.Other large sized Parts
LRTM General Design Guidelines
| Minimum Radius | 6 mm (0.236 in) |
| Minimum Draft | 2 degrees |
| Minimum Thickness | 3 mm (0.125 in) |
| Maximum Thickness | 12.7 mm (0.500 in) |
| Typical Reinforcement Loading | 30 – 40 % |
| Density (GP resin) | 1578 kg/m3 (0.057 lb/in3) |
| Die Lock (Reverse Draft) | No |
EXAMPLES OF LRTM&VARTM
Below are several examples of RTM Mold which we have designed and manufactured. Auto parts,electronics, packing, etc.
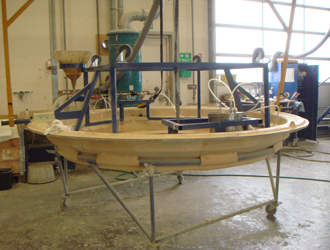


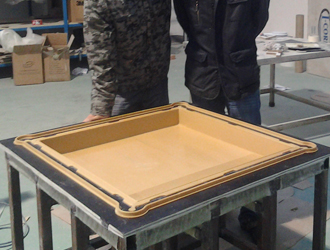
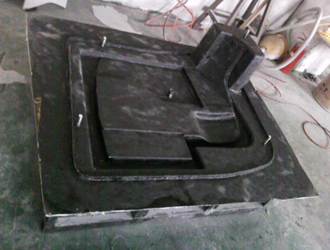
EXAMPLES OF LRTM&VARTM
Below are several examples of RTM products which we have designed and manufactured. Auto parts,electronics, packing, etc.
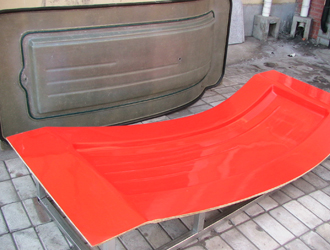

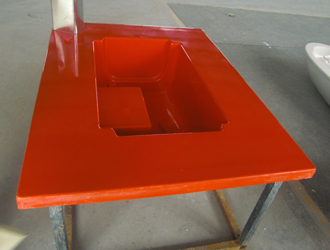

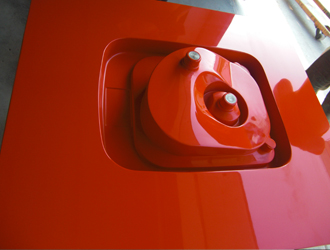

Do not hesitate to send us 3D files for analyze of the ability to mold these parts. We are ready to listen and to assist you in your plastic injection molding project.
86-13143415646
Contact:
 Tel: 86-755-23000620 Fax: 86-755-23000621
 Email:info@galaxy3dm.com/info@seetoptech.com
 Address: A3 , Dingfeng Industrial Zone, Fuyong Town, Shenzhen, China
Galaxy 3D Manfacturing Solution
Copyright (©) 2020 Shenzhen Seetop Technology Co.,Limited
