

UPVC Window and Door Profile Mould
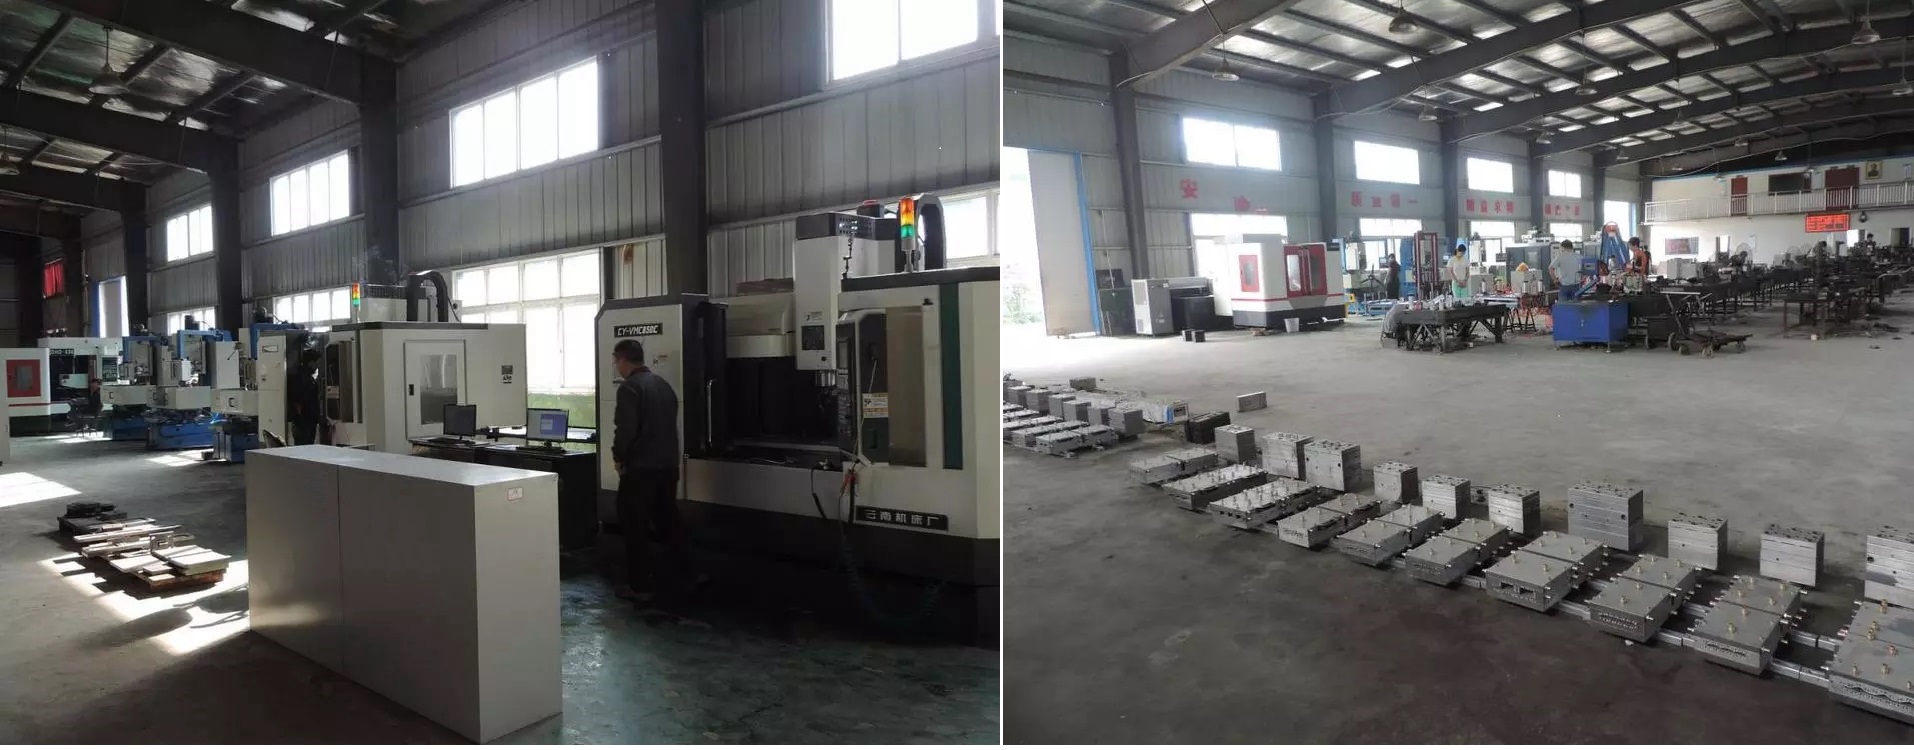
Extrusion MoldGalaxy3DM is a precision manufacturing factory located in Guang Dong. It is a professional manufacturer of cnc processing, 3D printing, stamping, sheet metal, aluminum & plastic extrusion, pressure die casting, silicone mold and injection molding.
Extrusion Mold
Extrusion moulding, or extrusion molding, is the molding of plastic or metals into a pre-defined shape.

Extrusion is a manufacturing process used to make pipes, hoses, drinking straws, curtain tracks, rods, and fibre. The granules melt into a liquid which is forced through a die, forming a long 'tube like' shape. The shape of the die determines the shape of the tube. The extrusion is then cooled and forms a solid shape. The tube may be printed upon, and cut at equal intervals. The pieces may be rolled for storage or packed together. Shapes that can result from extrusion include T-sections, U-sections, square sections, I-sections, L-sections and circular sections.
One of the most famous products of extrusion moulding is the optical fiber cable.
Extrusion is similar to injection moulding except that a long continuous shape is produced.

Extrusion Moulding: The Advantages
- Advantage – Low Cost
Extrusion molding has a low cost relative to other molding processes.This stems, in part, from the efficiency of the process. Most extrusion molding uses thermoplastics, which can repeatedly undergo melting and hardening. Leftover materials, normally discarded as waste in other processes, can be reused. This lowers raw material and disposal costs. Barring mechanical failure or planned downtime, plastic extrusion machines operate continuously. This reduces the chances of inventory shortage and allows for 24 hours-a-day manufacturing.
Advantage – Flexibility
Extrusion molding provides considerable flexibility in manufacturing products with a consistent cross-section. To picture a consistent cross-section, imagine cutting straight through a block of cheese in several places. No matter which pieces you pick up, they all maintain the rectangular block shape. So long as the cross-section remains the same, extrusion molding can produce complex shapes, such as decorative trims. With minor alteration to the process, manufacturers use extrusion molding for plastic sheets. Variation on the extrusion process also allow for the manufacturing of products that mix plastic attributes, such as hard and soft surfaces.
Advantage – Post-Extrusion Alterations
The plastic remains hot when it leaves the extruder, which allows for post-extrusion manipulation. Manufacturers take advantage of this and use a variety of rollers, dies and shoes to alter the shape of the extruded plastic to fit their needs.
Galaxy3DM is specialized in producing various UPVC, PVC, WPC, PE, PP, PS and other plastic extrusion mould.
As a professional extrusion mould manufacturer, through years of experience accumulation, we have created our own unique and complete theory of extrusion integrated system. We are in the leading level in the field of extrusion mould hot runner designing, plastic hot runner slight controlling, PVC low foaming technology, WPS raw material formula and extrusion operation technique, etc.

And our main products as follows:
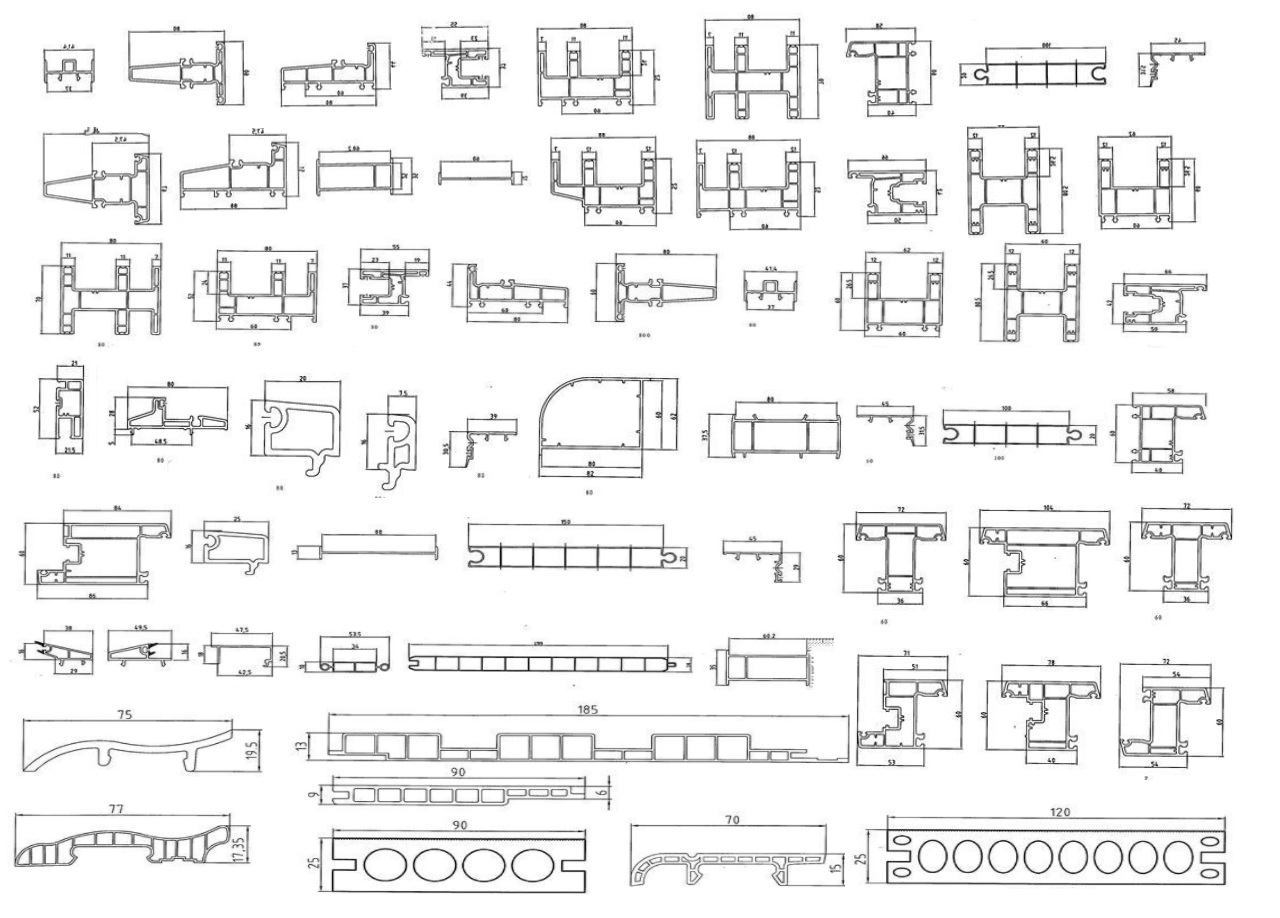
1. PVC plastic doors and windows (color co-extrusion, double-sided double-color co-extrusion, embossing and post co-extrusion) mould
2. PVC and PVC wood plastic door, wall panels, cabinet panels, window sill board, wall board and microcrystal floor moulds
3. PVC, PE wood plastic door series, floor and tray series moulds
4. Imitation marble stone plastic and foaming horn line moulds
5. PVC, WPC landscape fence and road traffic guardrails moulds
6. PVC, PE pipes (winding pipe, telecommunication pipe and drain pipe) moulds
7. Other profile (PVC trunking, rain gutter, soft PVC step plate) moulds
1. PVC plastic doors and windows (color co-extrusion, double-sided double-color co-extrusion, embossing and post co-extrusion) mould
2. PVC and PVC wood plastic door, wall panels, cabinet panels, window sill board, wall board and microcrystal floor moulds
3. PVC, PE wood plastic door series, floor and tray series moulds
4. Imitation marble stone plastic and foaming horn line moulds
5. PVC, WPC landscape fence and road traffic guardrails moulds
6. PVC, PE pipes (winding pipe, telecommunication pipe and drain pipe) moulds
7. Other profile (PVC trunking, rain gutter, soft PVC step plate) moulds
Welcome all of you to visit,we always try our best to create a famous brand and let our customers satisfied.
Our extrusion mould advantages:
1.we are founded in 2010, extend 10 years professional experennce gives us dominate position in extrusion moluld industry., quality and precision are the most import target of our company.our products enjoy an excellent reputation in plastic extrusion mould industry.
2.We owned a team of mature and experienced technicians,rich experiences skill workers from design, manufacture and debugging.
3.We can make all kinds of moulds according to customer requirement.The mould can be post-co extrusion, color co extrusion, embossing co extrusion, surface layer and so on.
4.Provide complete set of production process and technology transfer service
5. Flow channel systematic design is based on theoretical calculation, practical conclusion, adopting reasonable compressing ratio and stain technology.
We could give the whole support for customer in raw material formula, selection of extruder machine, mould technique and operation training on the spot.
We have research panel mould/WPC mould/PVC profile mould/industrial plastic mould, widely using in the industry of architecture material, decoration, door, window, household, daily necessities, environment, gardening and packing, etc.
Group of experts, hundreds of employees gather together, we can make what customer wanted and let it come true.
From our rich experiences, advanced equipment and perfect processing.
We have exported to dozens of countries and districts with high identification and mutual trust, such as Europe, America, Southeast Asia and Middle Asia, etc.
Standard Extrusion Mold Order Process
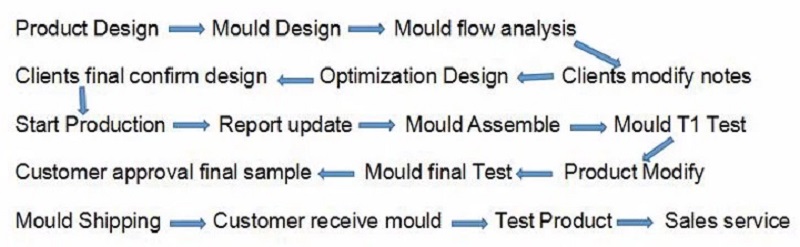
Clients' inquiry-Confirm Product design(material, size,weight,etc.)-Cient place order-Mould Design-Client confirm CAD Drawing-Start to Make mould-Report the Production Process-Mould testing-clients confirm testing result-packing-Delivery-Aftersale Service if needed

Production Introduction:
| Name | UPVC Window&Door frame extrusion mould with high accuracy |
| Size | Various types |
| Mould material | 3Cr17, 3Cr17MoNiV,or as per your request |
| Mould cavity | 1 or multi-cavity |
| Mould composition | Die head, aluminum heating bands, calibrators and water tank |
| Feature | Selectable co-extrusion of different raw materials: PVC, PP, PE, ABS |
| Selectable technology: low-foaming, high-foaming & substance co-extrusion | |
| Stable discharging, high efficiency, superior quality | |
| Test | Mould will be tested to get the satisfied sample before delivery |
| Service | Provide complete set of production process and technology transfer service |
| Lead time | 35-40 days |
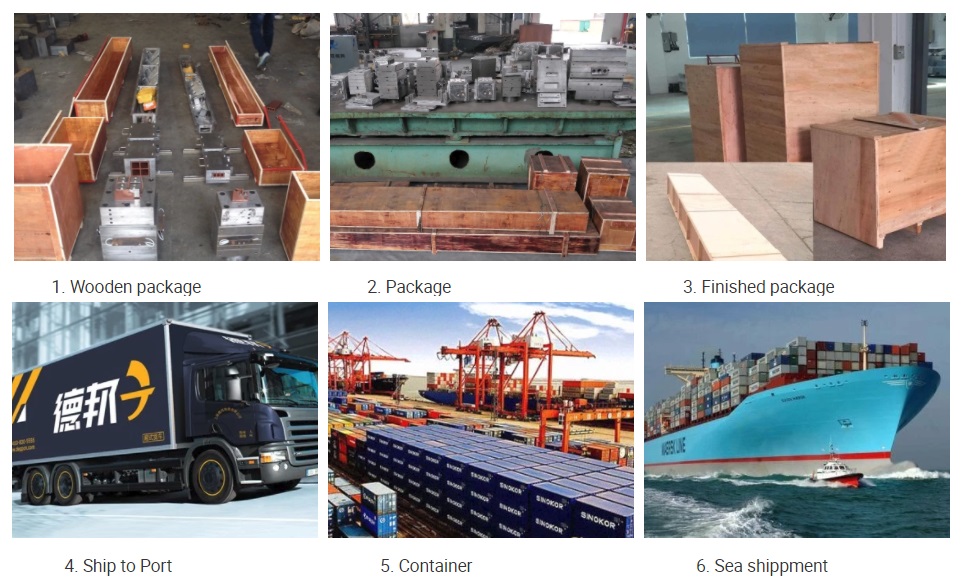
| Package | Wooden case for exporting, each mould will be cleaned before packaging. |
UPVC Window and Door Profile Mould Characters:
Window and Door Profile Mould Characteristics:
The extrusion die head design:
Use the removable positioning device, making it easier to disassemble.
Precise material flow control and stable extrusion.
The hidden heating design has increased the brightness of the product surface.
The special balance of the pressure holes has lowered the rejection rate.
The extrusion calibrator design:
The automatically adjusting positioning key gives it a precise size
The tapered design of the styling sets has increased the production speed greatly.
The inlet end is independent vacuum and shapes well.
The camber adjusting device ensures that the line is straight.
Extrusion cooling design:
Double vacuum system promotes the molding.
The combination design of eddy current and spray makes it cools fast..
The self-adjusting water tank panels are easy to adjust.
The stainless steel frame type system can prevent damage.
The special influent distribution gives it a cooling balance.

The Composition and Function of each part for UPVC Window and Door Profile Extrusion Mould :
| Configuration | Functions | Types |
| Dies head | Produce continuous,stable,homogeneous profile | Divided into four standards based on different appearances: D1602,D1802,D2002,D3002 |
| Calibrators | Cool down and form the profile, the smaller the resistance is ,the better | Divided into four standards based on different widths: C1402,C1702,C2002,C3002.The quantity of calibrator parts are decided by profile, and extrusion speed. |
| Water tank | Cool down the profile further | Divided into three kinds: organic glass, stainless steel, pp board. They have wonderful tightness, brief frame, easily be processed. |
Die ( plastic extrusion die/pvc profile extrusion die/pvc extrusion die )
1. Designed by different formulations and melt flow characteristics
2. Multi-cavity with material supplied to each cavity respectively,Smooth of flowing channel
3. Integated mandrel structure, Mirror polishing
Calibrator ( plastic extrusion die/pvc profile extrusion die/pvc extrusion die )
1. High efficient and even cooling system
2. A number of patented brightening technology
3. The perfect combination of precise positioning and reliable shape
Water tank ( plastic extrusion die/pvc profile extrusion die/pvc extrusion die )
1. Spraying and immersing cooling system
2. Vacuum and whirling water tank
3. Floating tank plates, Find position automatically
Product Test Result:
| NO. | Test Items | Technical Requirements | Units | Measured Value | Single Conclusion |
| 1 | Extrusion speed | 0.8-1.8 | m/min | 0.87 | conform |
| 2 | Yield | >98 | % | 99 | conform |
| 3 | Thickness deviation | <1.2 | mm | 0.24 | conform |
| 4 | Water absorption | ≤3.0 | % | 1 | conform |
| 5 | Density | ≥0.85 | g/ cm3 | 1.38 | conform |
| 6 | Tightness | No leakage | / | conform | conform |

Scope of application for Extrusion Mold:
Landscape construction, floor, wall panel, fence, panel, door panel, Industrial pallets, architecture decorative panel, foaming panel, pipe ect.

Fine quality after-sale service Policy:
1.Our company has high level of technology,rich experiences in testing mould and good reputation service team.
2.Principles of service:
First testing combined with tracking service
Orientation services linked with peripatetic service
Technical services united with training endorsement
3.Replying clients' problems in time ,and the technical can be arrived in three days.
4.One year warranty for the mould,and maintain for the whole life.
5.We can provide a whole set of technical support including extruder election, formula process and extrusion mould.
We give the whole support for customer in raw material formula,selection of extruder machine,mould technique and operation training on the spot.
6.we have excellent test mold technicians
7.All the moulds must be inspected and tested to reach 100% qualified before delivery.
9 We provide overseas technical service .
1. Quality control
After moulds are finished, we will test the moulds and offer samples to our customers for approval before delivery.
Product test results will be provided.
| NO. | Test Items | Technical Requirements | Units | Measured Value | Single Conclusion |
| 1 | Extrusion speed | 0.8-1.8 | m/min | 0.87 | conform |
| 2 | Yield | >98 | % | 99 | conform |
| 3 | Thickness deviation | <1.2 | mm | 0.24 | conform |
| 4 | Water absorption | ≤3.0 | % | 1 | conform |
| 5 | Density | ≥0.85 | g/ cm³ | 1.38 | conform |
| 6 | Tightness | No leakage | / | conform | conform |
2.Test Facility
All our tools are proven before dispatch in our Test Facility where we have Extrusion Lines including twin and single screw Extruders and Co-Extruders to prove all types of tooling. In addition our technicians are always available for final tuning in the Customer’s factory, which we prefer in order to give a complete service.

3.Packing&Delivery:
Packing Details : Wooden package for exporting
Delivery Details : 30 days after receive the down payment and confirm all details.
4. Common finished product defects analysis
| Product defects | Possible reasons | Handling methods |
| Extrusion mould distortion | Too short cooling time, not enough cooling for finished products | delay the cooling time |
| Too rapid speed for extrusion, forced pull to lead the distortion | Slow down the speed of extrusion die | |
| Finished product structure with defects | Modify the dies | |
| Too high temperature for die, poor cooling for finished products | reduce the mould temperature | |
| Knit line | Insufficient injection pressure, too slow injection speed, too small gate and flowing pipe | Increase the injection pressure and injection speed, modify the gate and flowing pipe. |
| Too low forming temperature and mould temperature | Increase temperature, increase back pressure or accelerate the rotating speed of screw | |
| Insufficient exhaust in interflow zone and no run-off pit | Fix exhausting holes in interflow zone and increase the number of run-off pits. | |
| Use too much release agent | Reduce to use release agent | |
| Poor luster of finished products | Too slow injection speed, insufficient pressure and low mould temperature | Increase the injection speed, injection pressure and mould temperature |
| Hydrosphere or grease pollution in the mould cavity | Clean it up | |
| Poor grinding of mould surface or too small gate and flowing pipe | Modify mould | |
| Insufficient injection quantity or water contained in the raw material | Increase the injection pressure and injection speed, delay the jetti | |
| Cracks of extrusion mould of finished products | Too low temperature of material or mould | Increase the temperature |
| Insufficient stripping lean or improper extrusion way | Modify the mould | |
| Too small gate | Modify the mould | |
| Insufficient stripping angle | Modify the mould | |
| Coarse surface of extruded finished products | Too low forming temperature | Increase the temperature, accelerate the rotating speed of screw |
| Too low mould temperature | Increase the mould temperature | |
| Surface blocks of extruded finished products | Not clean material pipes, contain wastes | Clean up material pipe |
| The additive articles such as color master batch are not done according to the requirements | look for the corresponding color master batch | |
| Insufficient extrusion quantity | Insufficient temperature for material pipe | Increase the temperature |
| Wastes in the gate or too low speed rate of screw | Clean up the gate or accelerate the rotating spped of screw | |
| Extrusion mould expansion of extruded products | Too low temperature of mould head or too fast rotating speed of screw | Increase the mould head temperature and reduce the rotating speed of screw |
| Too fast limited material | Adjust the limited material device | |
| Produce much gas when extruding | Too high melting temperature | Reduce the melting temperature |
| Wastes in the material pipe | Clean up the material pipe | |
| Pits of extruded products | Water contained in the raw material | Dry the material |
| Too high meting temperature, too fast rotating speed of screw | Reduce the meting temperature, and the rotating speed of screw |
Welcome to contact us for more details.
FAQ
Q: Are you trading company or manufacturer ?
A: We are factory.
Q: How long is your delivery time?
A: Generally it is 25-30 days after receive the 30%down payment.
Q: Do you provide samples ? is it free or extra ?
A: Yes, we could offer the sample for free charge but do not pay the cost of freight.
Q: What is your terms of payment ?
A: Payment<=1000USD, 100% in advance. Payment>=1000USD, 30% T/T in advance ,balance before shippment.
Q:What is your main market?
A:Our market spread all over the world.
Q: How can you ensure the quality of mould:
A: We will test the mould before shippment.if you still worried about the quality,you can send us the material formula or examine the mould to our factory.


 复制产品链接
 长按图片保存/分享
询盘
咨询表单:
咨询内容:
你还没有添加任何产品

询盘
咨询表单:
咨询内容:
你还没有添加任何产品
86-13143415646
Contact:
 Tel: 86-755-23000620 Fax: 86-755-23000621
 Email:info@galaxy3dm.com/info@seetoptech.com
 Address: A3 , Dingfeng Industrial Zone, Fuyong Town, Shenzhen, China
Galaxy 3D Manfacturing Solution
Copyright (©) 2020 Shenzhen Seetop Technology Co.,Limited
